
blog
SEROX-W Process: Advanced Treatment of Sulfur-Containing Alkaline Wastewater with IVKAZ-W Catalyst

Introduction
Treatment of Refinery Sulfur-Containing Wastewater by Catalytic Oxidation Technology
Alkaline wastewater generated in refinery and petrochemical units commonly contains reactive sulfur compounds such as sulfides, hydrosulfides, sulfites, and mercaptides. Due to their toxicity, unpleasant odor, corrosive effects, and environmental restrictions, these compounds must be treated before the wastewater is sent to final treatment facilities.
The SEROX-W process has been developed as an advanced solution for the treatment of sulfur-containing alkaline wastewater.
This technology is based on catalytic oxidation in the liquid phase using the proprietary IVKAZ-W catalyst.
During the process, hazardous sulfur compounds are converted into more stable and less harmful products, including:
Dialkyl disulfides (RSSR)
Sodium sulfate (Na₂SO₄)
Sodium thiosulfate (Na₂S₂O₃)
SEROX-W Process
The SEROX-W process is a catalytic oxidation technology designed for the treatment of sulfur-containing alkaline wastewater.
The feed to the process may contain compounds such as:
Hydrogen sulfide (H₂S): from oil and gas processing units
Sodium sulfide (Na₂S): from spent alkaline solutions
Hydrosulfides: from hydrocarbon sweetening processes
Sulfites: from sulfur-containing process streams
Sodium mercaptides: from demercaptanization units
SEROX-W Process Mechanism
Wastewater Transfer and Preparation
After residual hydrocarbons, suspended solids, and mechanical impurities have been separated, the sulfur-containing alkaline wastewater is transferred to vessel V-1.
The wastewater is then pumped by P-1 and passed through heat exchangers H-1 and H-2 before entering the main process reactor.
IVKAZ-W Catalyst Injection
Before the wastewater enters the reactor, the IVKAZ-W catalyst solution is added to the stream through a controlled dosing system.
The catalyst accelerates the oxidation reactions of sulfur-containing compounds.
Oxidation Reaction in the Reactor
The oxidation of sulfur compounds takes place in reactor R-1.
Typical process operating conditions are:
Operating temperature: 40–65°C
Pressure: 0.4–0.5 MPa
Catalyst: IVKAZ-W
Oxidizing agent: Compressed air
Main Chemical Reactions in the SEROX-W Process
Oxidation of Sodium Sulfide
3Na₂S + 4O₂ + H₂O → Na₂S₂O₃ + Na₂SO₄ + 2NaOH
Oxidation of Sodium Mercaptide
2RSNa + 0.5O₂ + H₂O → RSSR + 2NaOH
SEROX-W Process Flow
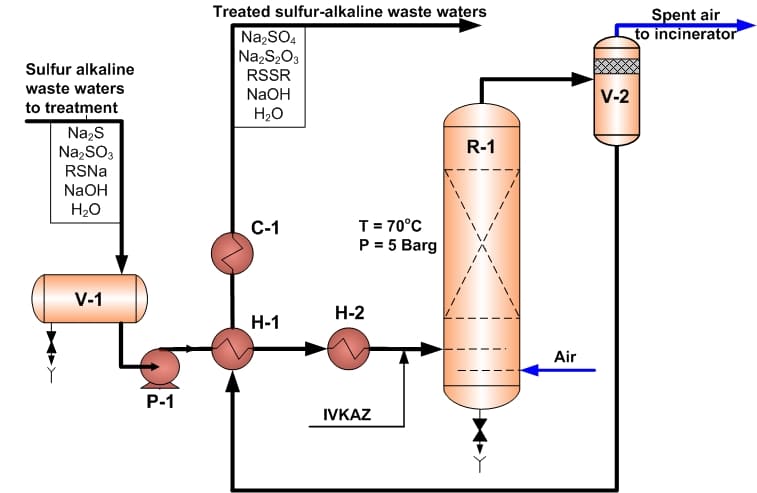
In the SEROX-W process, sulfur-containing alkaline wastewater is preheated and mixed with the IVKAZ-W catalyst before entering the oxidation reactor.
Compressed air is introduced from the lower section of the reactor, allowing sulfur-containing compounds in the wastewater to be oxidized into more stable products.
After the reaction stage, the spent air is separated in vessel V-2 and routed to an incineration system. The treated wastewater is then cooled and transferred to downstream treatment units for further processing.
Performance and Efficiency of the SEROX-W Process
The SEROX-W process is capable of achieving high removal efficiencies for sulfur compounds present in alkaline wastewater.
According to process data, the removal efficiency of sulfides and mercaptides can reach up to 99.9%.
Industrial Operating Experience
The SEROX-W process has been implemented in various industrial refinery applications.
Ryazan
In operation since: 1990
Application: Treatment of sulfur-containing alkaline wastewater
Yaroslavl
Operating period: 1995–1996
Application: Treatment of sulfur compounds
Kuibyshev
Operating period: 1995–1996
Application: Treatment of alkaline wastewater
The technology has also been applied in process units associated with cracking operations and alkaline wastewater treatment at JSC LUKOIL-Neftekhim in Burgas, Bulgaria.
Advantages of SEROX-W Technology
The main advantages of this process include:
Effective reduction of toxic sulfur compounds
Regeneration of spent alkaline solution
Reduction of pollutant load on biological wastewater treatment units
Reduced generation of hazardous sulfur-containing waste
Mild operating conditions
Use of the proprietary IVKAZ-W catalyst
IVKAZ-W Catalyst and Its Applications
IVKAZ-W is a specialized catalyst developed for the oxidation of sulfur-containing compounds in alkaline media.
It is part of the IVKAZ catalyst family and has been developed for applications including:
Crude Oil and Gas Condensate Treatment: Removal of H₂S and mercaptans
LPG Treatment: Reduction of sulfur compounds
Straight-Run and FCC Gasoline Treatment: Reduction of mercaptan sulfur
Light Hydrocarbon Fraction Treatment: Removal of mercaptans
Sulfur-Containing Alkaline Wastewater Treatment: Oxidation of sulfides and mercaptides
Ammonia-Catalytic Processes: Treatment of heavy crude oils
Industrial Experience with IVKAZ Catalyst
IVKAZ catalyst has been used in more than 40 industrial units based on VNIIUS technologies in Russia and other countries.
Countries with operating experience using this technology include:
Iran
Bulgaria
Latvia
Lithuania
The Netherlands
In addition, the catalyst has been used since 1994 in demercaptanization units at the Tengizchevroil gas-processing complex in Kazakhstan.
Conclusion
The SEROX-W process is an effective technology for the treatment of sulfur-containing alkaline wastewater. By using the proprietary IVKAZ-W catalyst, the process enables the catalytic oxidation and removal of sulfur compounds such as sulfides and mercaptides.
In addition to reducing the environmental pollutant load, the technology can support the regeneration of spent caustic and help reduce the overall cost of downstream wastewater treatment.
AAprolab
AAprolab serves as the exclusive representative for the production of IVKAZ catalyst under license from VNIIUS and IVKAZ, Russia. Through the supply of IVKAZ catalysts and associated process technologies, AAprolab provides specialized solutions for the refining, petrochemical, and gas-processing industries.